Bragan Ingredients explains how colour transcends mere appearance to ensure brand consistency, product appeal, and effective market differentiation strategies.

Today, it goes beyond mere appearance – colour ensures brand consistency, product appeal, and market differentiation. From processed foods to beverages, bakery, dairy, and confectionery, the use of vibrant, stable colours is central to producing products that attract attention on the shelf and maintain consumer trust.
Colour as a key component
In industrial food production, colour is not just decorative – it is functional and strategic. Consistent, high-quality colours help products look appealing and maintain uniformity batch after batch. Primary and lake colours remain essential in delivering bright, stable, and long-lasting hues, while natural colourants are increasingly used to meet consumer demand for clean-label products.
Primary vs lake colours
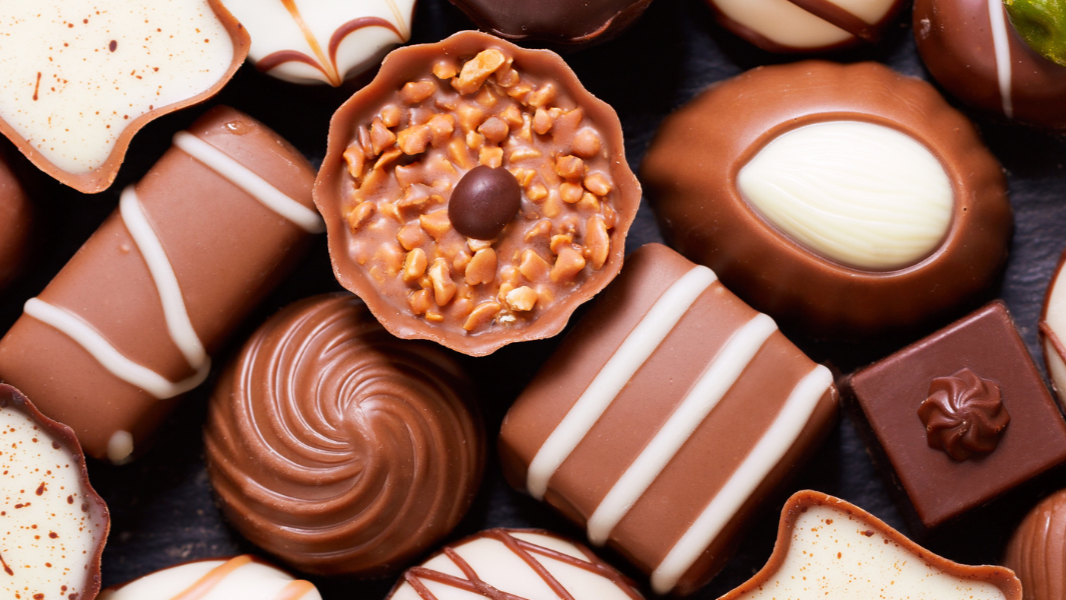
Primary colours are water-soluble and ideal for applications such as beverages, syrups, and dairy products, where even dispersion is key. Lake colours, on the other hand, are oil- or fat-soluble, making them perfect for dry mixes, chocolate, confectionery, and baked goods. Lakes provide greater stability in fat-based or low-moisture environments and prevent colour migration during storage or processing. By combining primary and lake colours strategically, manufacturers can achieve consistent, vibrant results across a wide range of product types and production processes.
Whether in candies, beverages, baked goods, or processed meals, precise colouring ensures product reliability. Consumers expect the same visual experience every time they purchase a product, and manufacturers rely on colour to deliver that consistency. Stable colourants also help protect products from fading during storage or transport, ensuring a professional and appealing look from production line to retail shelf.
The consumer and market impact
Consumers are drawn to products that look appealing and align with their expectations. Vibrant colours signal freshness, flavour, and quality, influencing purchasing decisions in highly competitive markets. Beverages, snack foods, dairy products, and confectionery all benefit from consistent and attractive colouring, which can make products more memorable and encourage repeat purchases. Colour also plays a crucial role in brand recognition.
Distinctive and consistent colour palettes help products stand out on crowded shelves and reinforce brand identity. For manufacturers, this is more than aesthetics – it’s a key component of marketing and product strategy. As the demand for visually appealing foods grows, manufacturers are increasingly combining traditional synthetic colourants with natural and plant-based options. This approach balances visual impact, regulatory compliance, and consumer preferences for clean-label ingredients.

Colour as a strategic ingredient
In food manufacturing, colour is no longer an afterthought – it is an essential ingredient in product design and consumer engagement. From shelf appeal to brand recognition, the skilful use of primary and lake colours, along with innovative natural alternatives, ensures products meet both aesthetic and market expectations. Discover how Bragan Ingredients can partner with you to achieve consistent, vibrant, and market-ready products using our range of primary and lake colours.
